MIG and TIG are two widely used arc-welding processes, and both can produce strong, high-quality joints in steel. However, they create and control the weld in different ways. MIG is generally associated with speed and productivity, while TIG gives the welder very precise control and can produce exceptionally neat results.
Neither method is automatically better. The right choice depends on the steel thickness, joint design, required finish, production volume, working conditions and applicable welding procedure.
At GLW Engineering, our team specialise in steel fabrication services, welding, and so much more. Give us a call today!
How MIG welding works
MIG stands for metal inert gas, although the process for ordinary carbon steel often uses a gas mixture and may technically be described as MAG welding. In everyday workshop language, “MIG” is commonly used to refer to both.
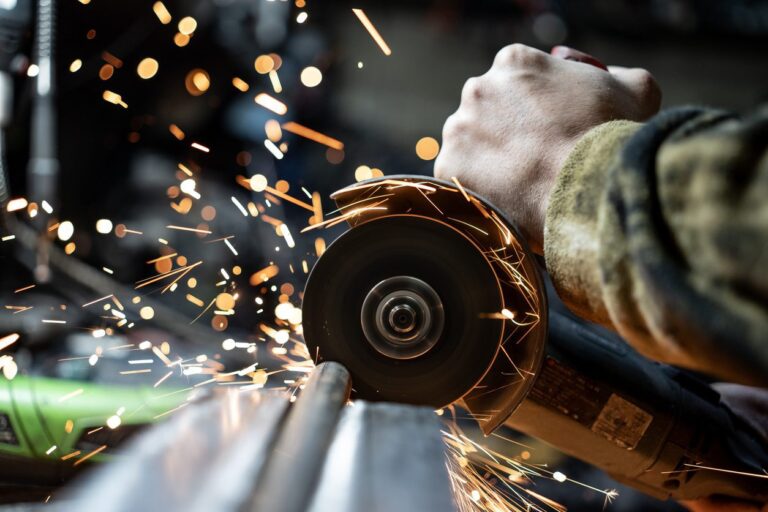
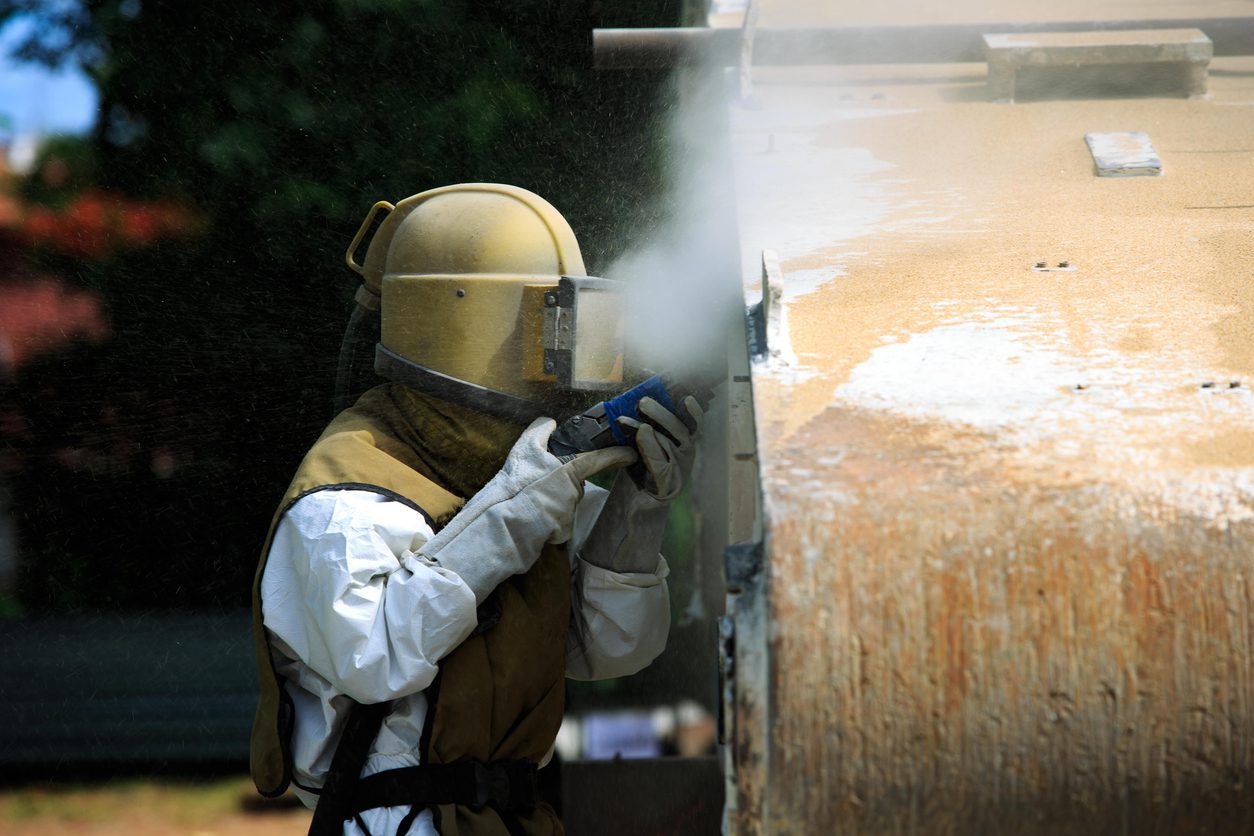
A welding machine continuously feeds a wire electrode through the torch. An electric arc forms between the wire and the workpiece, melting both the wire and the steel edges. Shielding gas flows around the arc to protect the molten weld from atmospheric contamination.
Because the filler wire is fed automatically, the welder can create a continuous weld without repeatedly stopping to add material.
This makes the process efficient for general fabrication.
Where MIG welding performs well
MIG welding is used extensively for frames, structural components, brackets, platforms, gates and production fabrication. It can be applied to a broad range of thicknesses, provided the machine, wire, gas and settings are appropriate.
The process offers relatively high deposition rates, meaning filler metal can be added quickly. That is valuable for longer welds or projects containing many similar joints. It is also easier to learn at a basic level than TIG, although producing consistently compliant welds still requires training, practice and proper control.
MIG equipment settings include voltage and wire-feed speed. These must be balanced with travel speed, material thickness and joint preparation. Incorrect settings can lead to problems such as a lack of fusion, excessive spatter or burn-through.
How TIG welding works
TIG stands for tungsten inert gas. The arc forms between the workpiece and a non-consumable tungsten electrode held in the torch. If filler material is needed, the welder adds a separate rod by hand while controlling the torch.
Shielding gas, usually argon or an appropriate mixture, protects the electrode and weld pool. Because the heat source and filler addition are controlled separately, the welder can make fine adjustments as the weld develops.
This demands coordination and usually makes TIG slower than MIG. The workpiece must also be prepared carefully because TIG is less tolerant of rust, oil, paint, and other contaminants.
Where TIG welding performs well
TIG is well-suited to work requiring clean, controlled welds and a high-quality appearance. It is often used for thin material, intricate joints and visible architectural work. It is also a common choice for stainless steel and non-ferrous metals, though it can be used very effectively on carbon steel.
The process produces little spatter and gives close control over heat input. This can help when welding thin components where excessive heat would cause distortion or burn-through.
However, TIG’s slower travel and filler deposition can make it less economical for long, heavy welds. It also performs best in a controlled environment, as draughts can disrupt the shielding gas.
Comparing speed and productivity
MIG is usually faster. The continuously fed wire and ability to deposit filler efficiently make it a practical option for repeated production and substantial fabricated assemblies.
TIG is more deliberate. The welder controls the arc and filler separately, which can improve precision but increases the time needed for each joint. Where labour time significantly affects cost, this difference matters.
Speed should not be considered on its own. If a visible MIG weld would require extensive dressing to achieve the specified appearance, TIG may still make sense. Conversely, choosing TIG purely because it looks refined can add unnecessary time when a MIG weld already meets every technical and visual requirement.

Comparing appearance and clean-up
A skilled operator can produce neat welds using either process. TIG is especially associated with a smooth, controlled bead and minimal spatter. It can be attractive on exposed steelwork where the weld remains visible.
MIG welds can also be clean, but spatter is more likely and may need to be removed before painting or powder coating. The appearance depends on preparation, settings, access and welder technique.
Grinding every weld flush is not automatically desirable. Removing too much metal can reduce the effective joint, while unnecessary dressing adds cost. The finish should be agreed during design, with structural performance taking priority where relevant.
Comparing steel thickness and joint type
TIG’s heat control makes it valuable for thinner gauges and delicate joints. MIG can also weld thin steel, but settings and technique must be carefully chosen to avoid distortion.
For thicker sections, MIG generally offers greater productivity. Multiple passes may still be required depending on the joint and welding procedure. Proper edge preparation helps the weld penetrate the full area it is intended to join.
Access and welding position also influence the decision. A method that works efficiently on a bench may be less convenient in a confined space or during site installation.
Weld quality depends on more than the process
A weld is not good merely because it was made using TIG, nor is it unsuitable simply because MIG was chosen. Quality comes from suitable joint design, compatible consumables, clean material, correct settings, qualified personnel and inspection.
For regulated or structural work, welding should follow the relevant procedures and execution requirements. The specification may determine which process, filler and inspection regime can be used.
The choice is therefore an engineering and production decision, not a simple contest. MIG typically provides speed and versatility for general steel fabrication, while TIG offers exceptional control for precise or visually sensitive work. Experienced fabricators may use both processes on different parts of the same project.
If you want to learn more about steel fabrication, our team at GLW Engineering are more than happy to help. Give us a call today!